
Electron beam welding
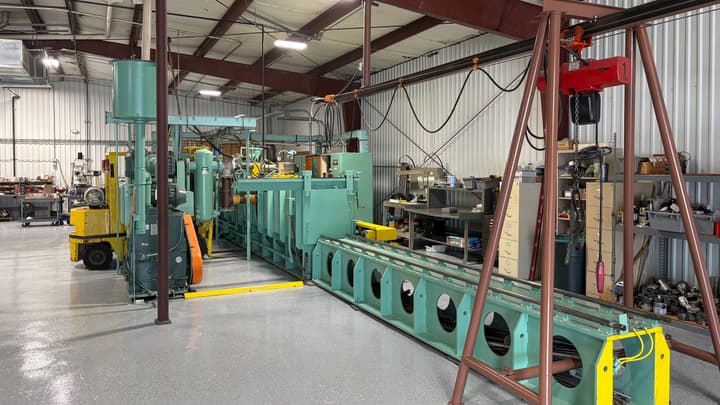
Rotary and linear EB welds from 0.010" to 6" deep on three machines, including a 42 kW CNC Sciaky for parts up to 23.5 ft long.
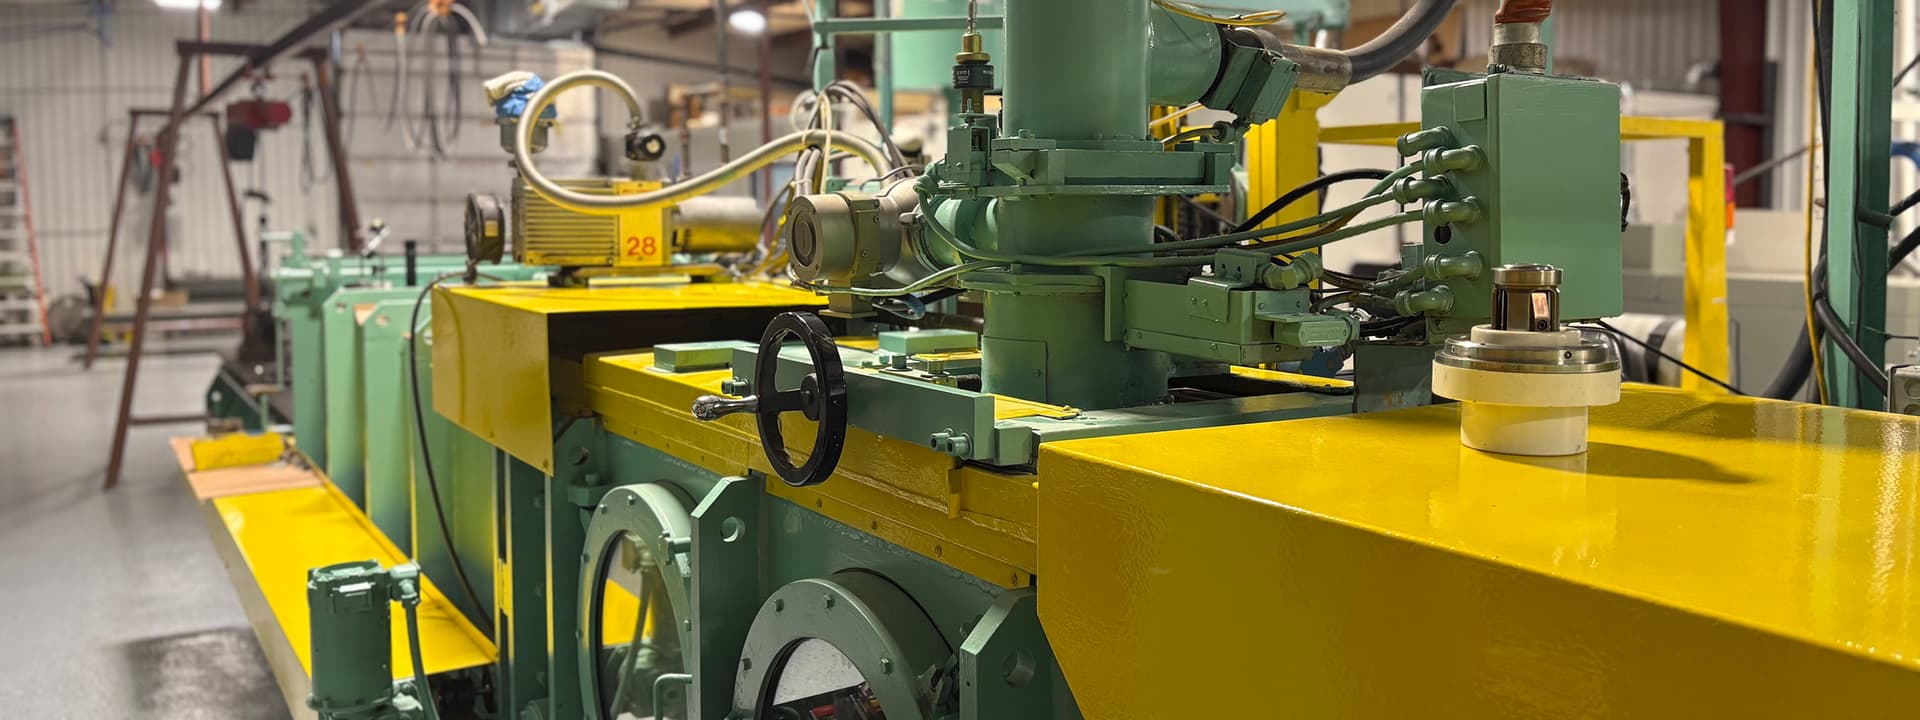
CNC electron beam welding for downhole tools and sensor housings
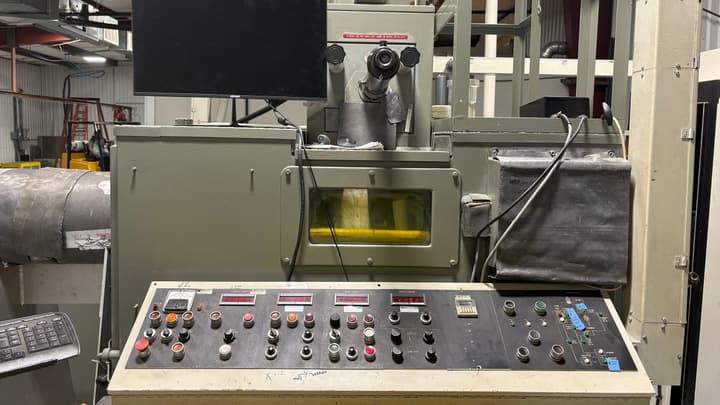
Welding is all we do. Our three electron beam machines cover penetration from 0.010" to 6", and every weld is made in a vacuum chamber with no filler metal or shielding gas. On the CNC Sciaky, all welding parameters are programmed, joint axis correction included, so each part in a run gets the same recorded settings.
Most of our work is for oil and gas: downhole tool housings and the sensor and instrument assemblies that go downhole with them, into high-pressure, high-temperature service. Major oilfield service companies list us as an approved EB welding vendor. We weld anything from a few prototypes to large production runs.
- 0.010"–6" Penetration range
- To 23.5 ft Part length (joint-dependent)
- 42 kW CNC Sciaky
- 1 day Typical quote
What we weld
Circumferential welds
Rotary welds on tool housings, probes, gauges, plugs, and sensor housings.
Straight-line welds
Linear joints, CNC-controlled from start to finish.
Constant or variable penetration
Depth held steady along the joint, or changed where the drawing calls for it.
Dissimilar metals
Many combinations can be joined when the materials are compatible.
Close to heat-sensitive parts
Low heat input lets welds sit near O-rings, plastics, and electronic components.
Design and fixturing help
Support with part design, tooling, fixturing, and metallurgy before the first weld.
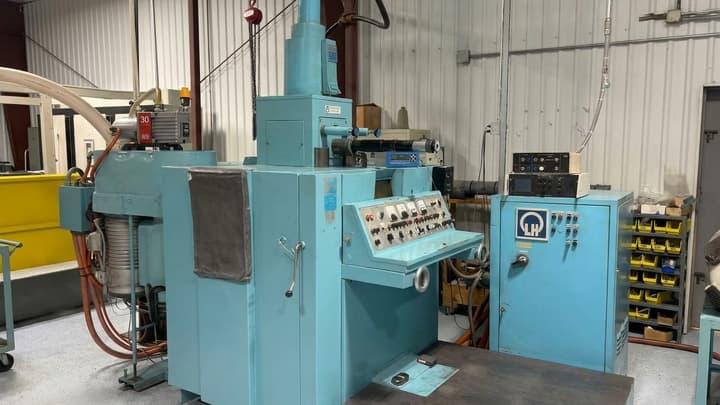
Three electron beam welders
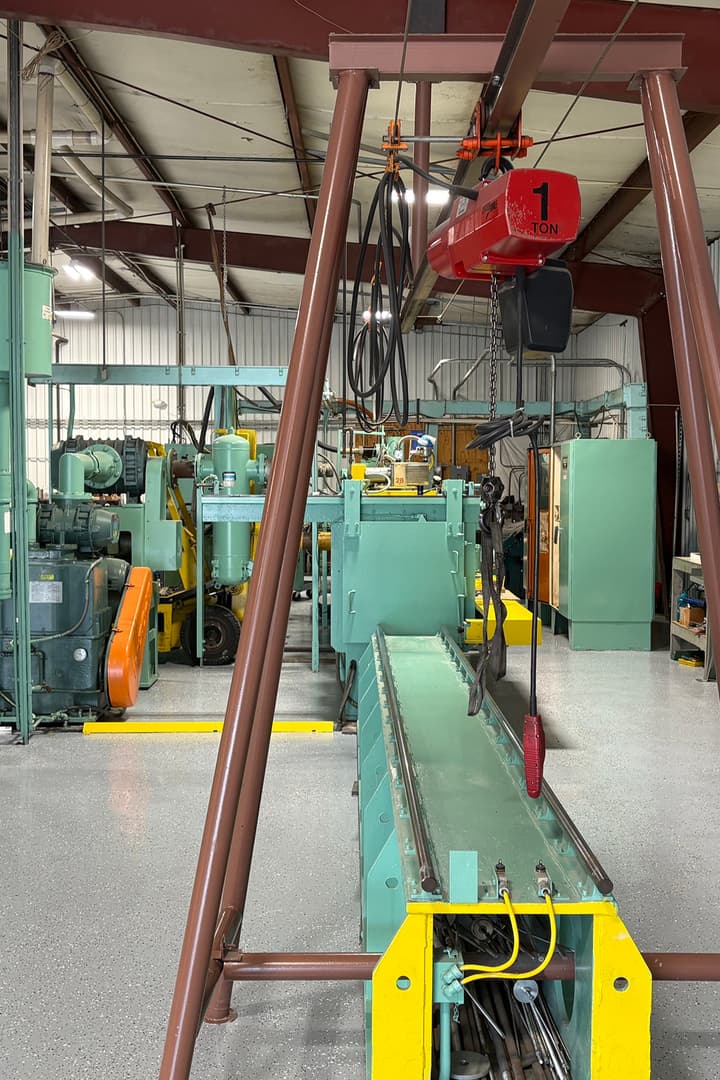
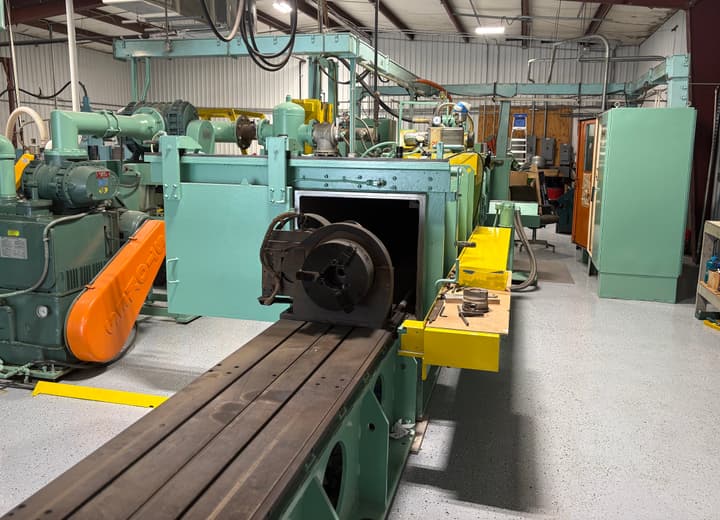
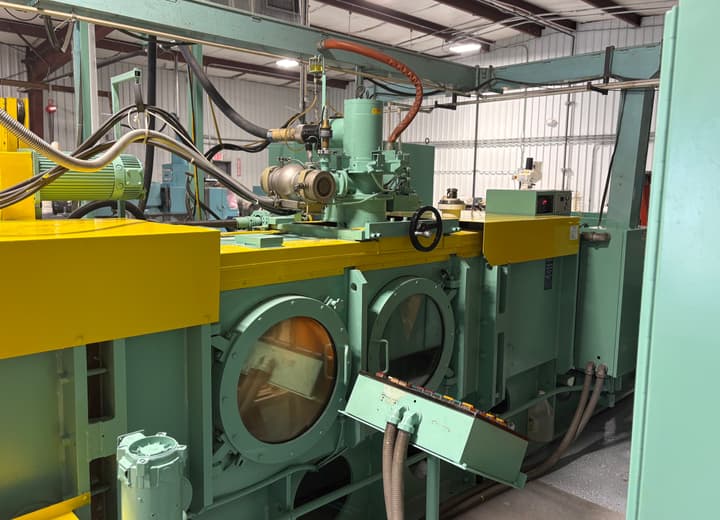
Our 60 kV, 42 kW CNC Sciaky is one of the most powerful CNC electron beam welding machines in Texas, built for long, heavy parts and welds up to 6" deep. Two 150 kV machines, the Leybold Heraeus and the PTR, handle small, precise welds from 0.010" deep.
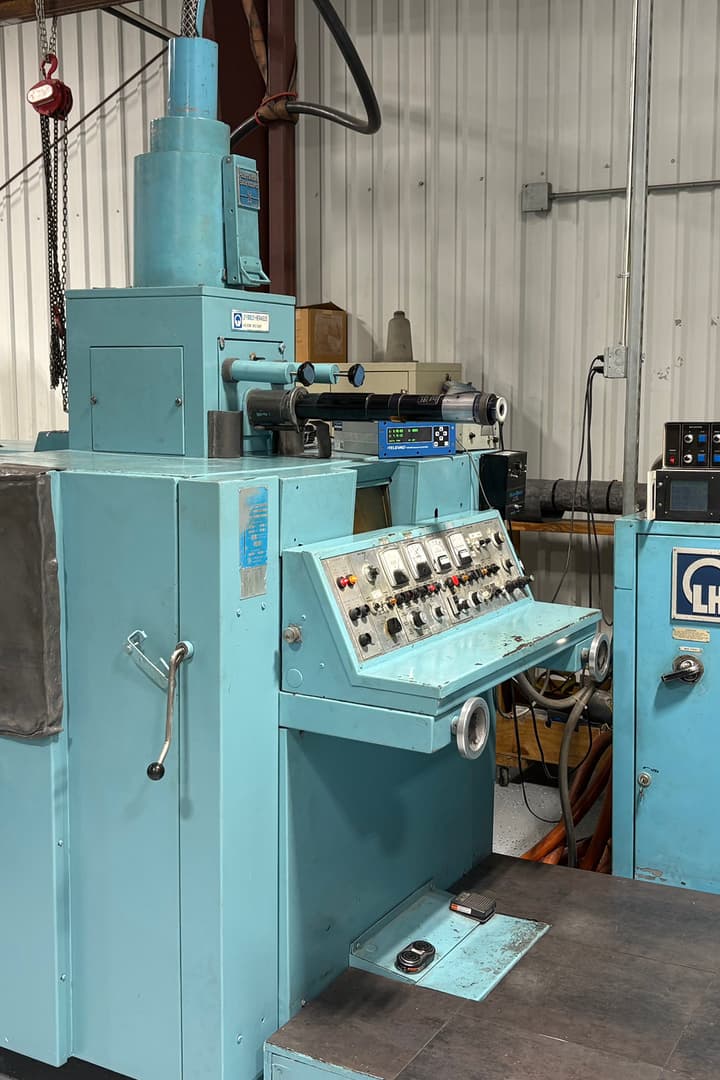
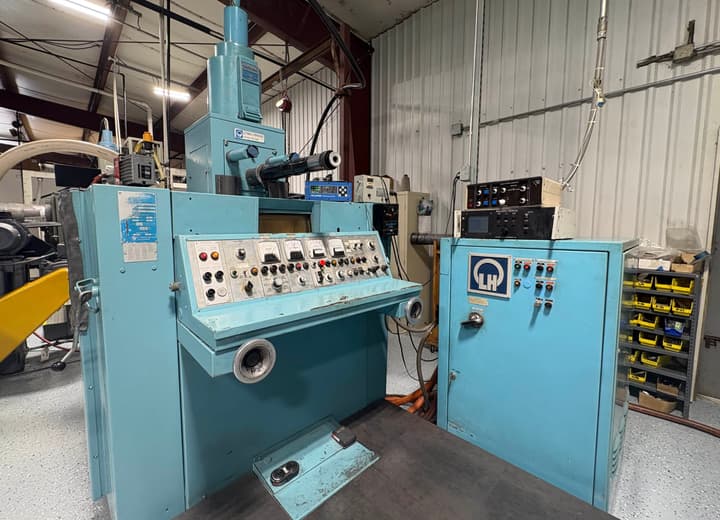
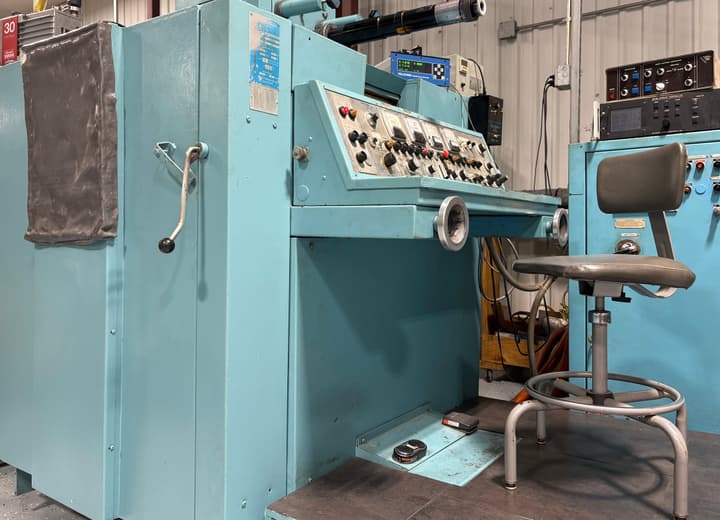
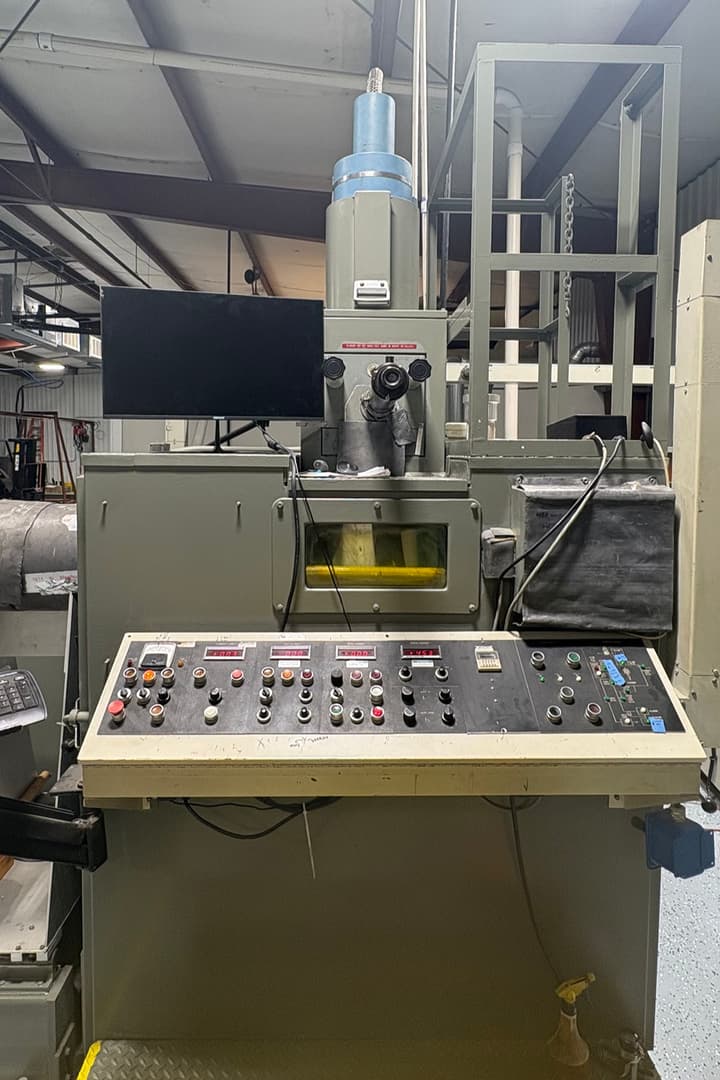
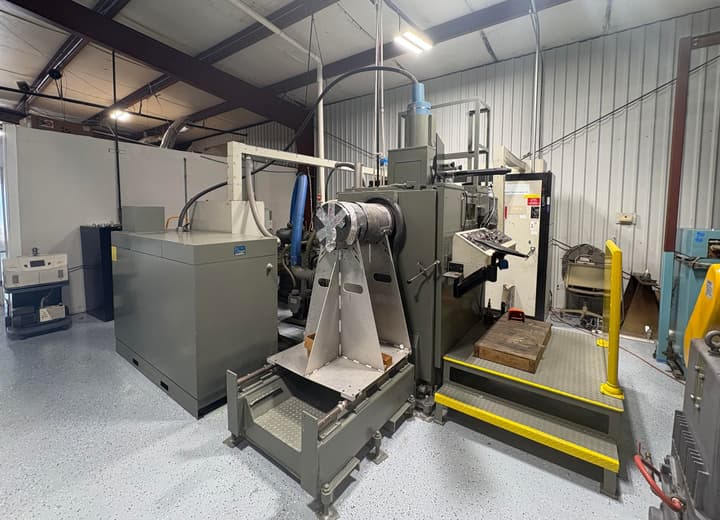
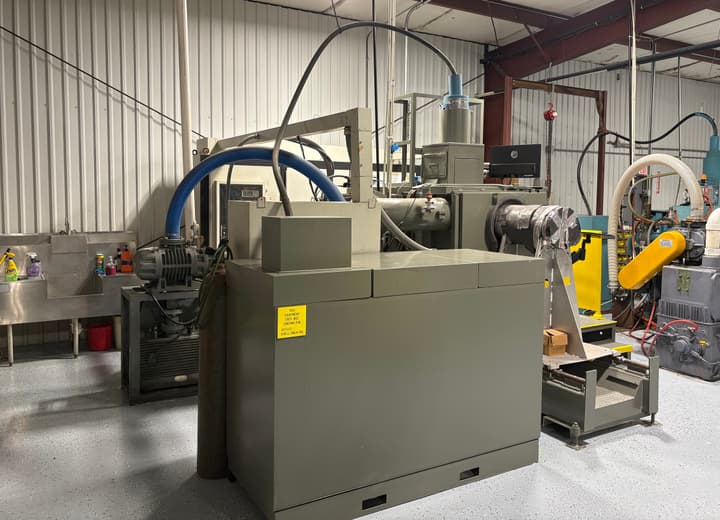
Welding range across three machines
- Penetration range
- 0.010" to 6", depending on machine
- Sciaky
- 60 kV · 42 kW · CNC · .200" to 6" penetration
- Part length
- To 23.5 ft, depending on joint location (Sciaky)
- Weld diameter
- To 11" (Sciaky) · to 3.5" (Leybold Heraeus)
- Leybold Heraeus and PTR
- 150 kV · 0.010" to 1.00" penetration
- Batch and tall parts
- 24-chuck Ferris wheel fixture (Leybold Heraeus) · deflection welding for parts up to 37" tall and 5" in diameter (PTR)
Materials we weld
- Inconel
- Incoloy
- Hastelloy
- Titanium
- MP35N
- Beryllium copper
- Nitronic 50
Many dissimilar-metal combinations can be EB welded when the materials are compatible. See materials and dissimilar metals.
How an EB welding job runs
Send your print
Email or upload the drawing showing the weld location, depth, and tolerance.
Get a quote
Quotes typically come back within 1 day.
Sample weld for new parts
We weld a test piece, then cross-section, polish, and etch it and send it to you to check. Once you approve it, we record the parameters as a WPS.
Production welding
Parts are welded with the recorded parameters, usually in about 1–2 weeks. Expedite is 2–3 business days, quantity permitting.
Quality tracking form
Each shipment includes a form recording the part identification, how it was welded, and any problems noted before and after welding.
Electron beam welding questions
What do you need to quote my part?
The drawing with the EB weld callout: weld location, depth, and tolerance. Add the material, quantity, and need-by date, and tell us if you need it expedited.
How fast can you turn parts around?
Quotes typically take 1 day, and standard production takes about 1–2 weeks. Expedite is available in 2–3 business days, quantity permitting.
How large or deep a weld can you make?
Penetration runs from 0.010" to 6", depending on the machine. The Sciaky welds parts up to 23.5 ft long, depending on joint location, with weld diameters up to 11". For example, we welded an 8-1/2" diameter beryllium copper part, one of our own shop designs, 2.2" deep.
Does my part need special preparation?
The part has to fit in the vacuum chamber, and the joint needs tight fit-up and fixturing; magnetic materials may need demagnetizing first. We typically help with joint design, tooling, and fixturing before welding, and the joint design guide shows common joint types.
Process, equipment, and quality
Weld process development
Sample welds for new alloys and combinations, evaluated before production.
How we develop a weldEquipment and capabilities
Full specs for all three electron beam welders, the spot welder, and the helium leak detector.
Full equipment specsQuality and qualification
Sample weld, your approval, a recorded WPS, and a quality tracking form with every shipment.
Our quality process
Send us your print
Quotes are typically returned within 1 day. Include the material, quantity, and the date you need the parts.
PDF · DWG · DXF · STEP · JPG · PNG
- Phone (713) 690-2326
- Email info@beamweld.com