
Electron beam welding services in Houston, Texas
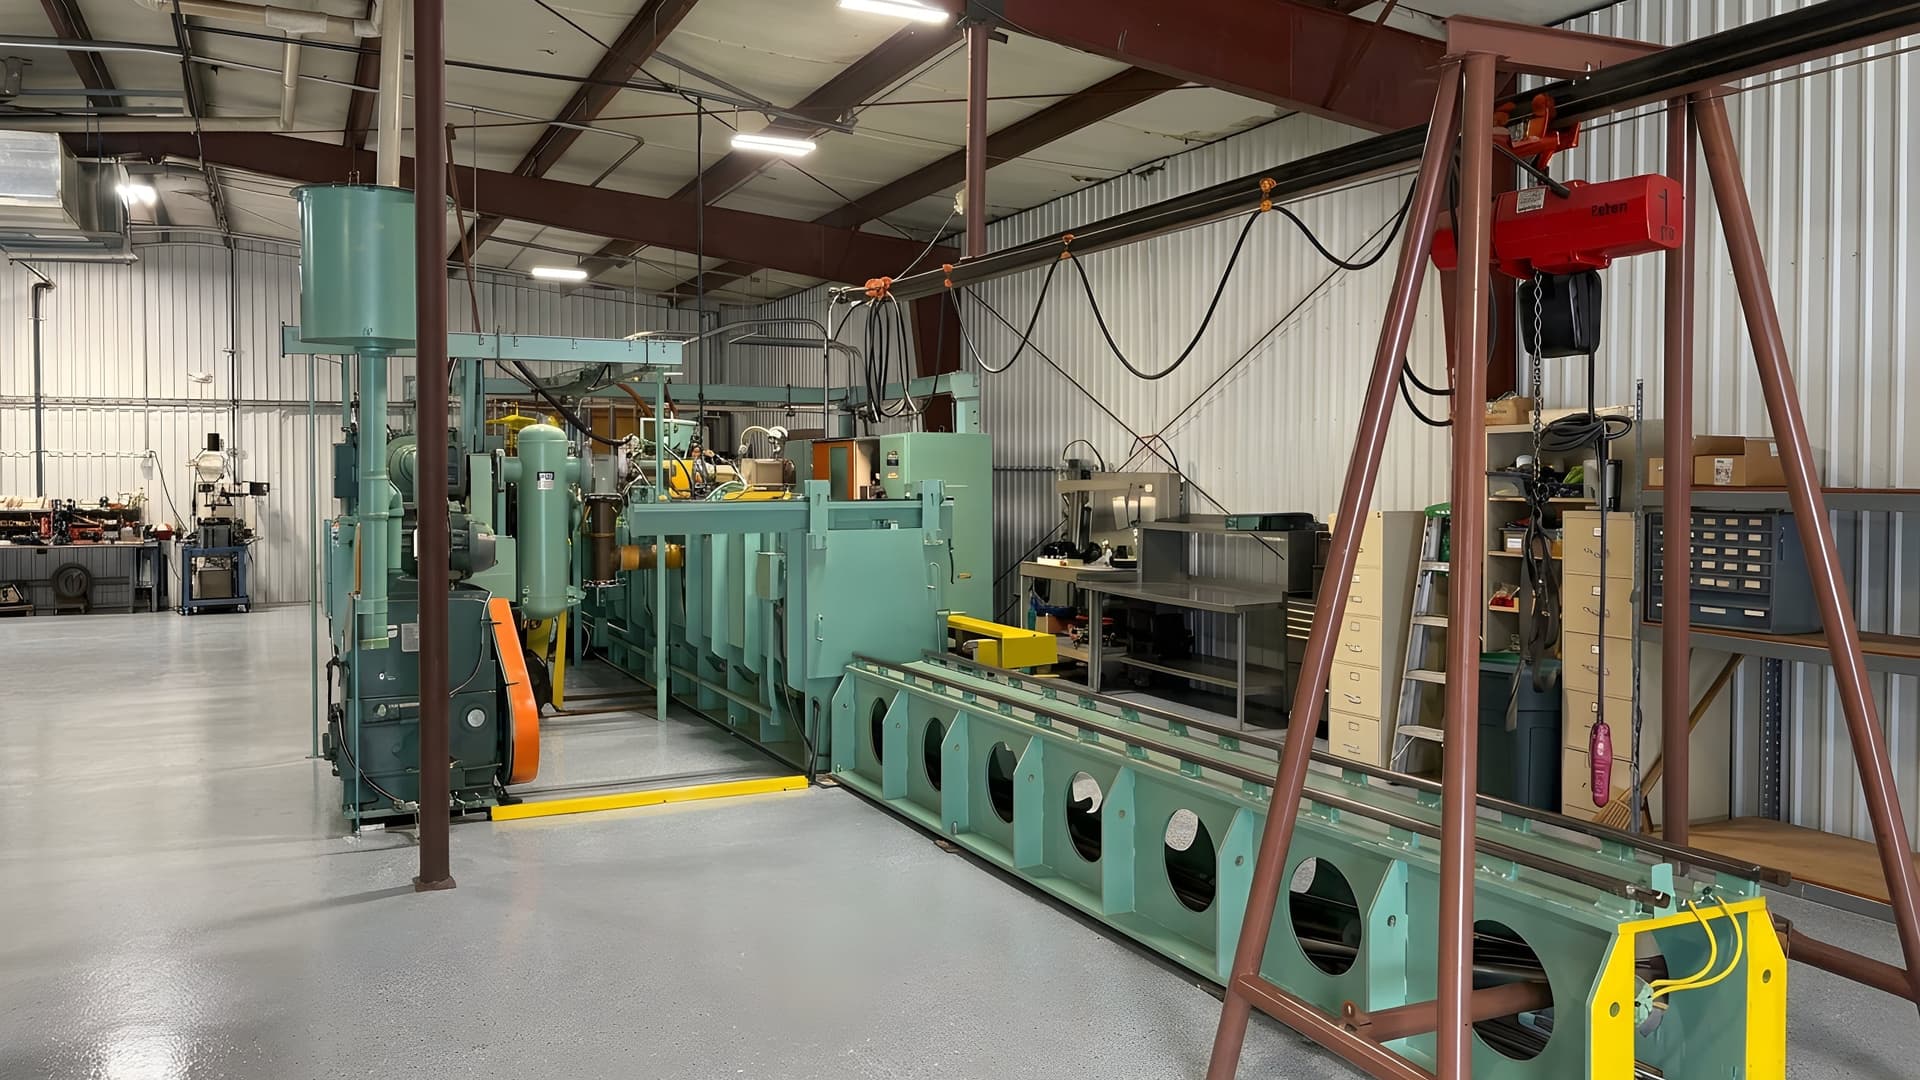
Our three electron beam welders include a 42 kW CNC Sciaky, one of the most powerful CNC electron beam welding machines in Texas. We weld prototypes through large production runs.
Have a print ready to quote?
Send Your PrintIs electron beam welding right for my part?
See the joint design guideOr email your print to info@beamweld.com
- Penetration 0.010"–6"
- Part Length To 23.5 ft
- Weld Diameter To 11"
- Among the Most Powerful CNC EBW in Texas 42 kW
- Quotes Typically 1 Day
Our welding and testing services
We weld circumferential (rotary) and straight-line joints with constant or variable penetration, in similar and dissimilar metals. Jobs run from small prototype quantities to large production runs. Before welding, we typically help the design engineer with design, tooling, fixturing, and metallurgy.
- Penetration 0.010" to 6", depending on machine
- Parts up to 23.5 ft long
- Dissimilar metals, when compatible
- Prototypes to large production runs
Our Miyachi Unitek resistance spot welder controls current, pressure, and weld time. We use it to spot weld filter screen material, and we also quote other parts that need precision resistance spot welds. Some of the screens we fabricate go into downhole oil tools to filter hydraulic fluid, and we can help design and fabricate fine-mesh filter screens.
- Miyachi Unitek resistance spot welder
- Other spot-welded parts quoted on request
- Filter screens for downhole tools
- Fine-mesh screen design and fabrication
After welding, we seal the welded area with the fixture and O-ring that part needs, then run a helium leak test to confirm the weld is hermetic. The test is non-destructive. Helium is a small, inert tracer gas, and a mass-spectrometer leak detector picks it up at very low leak rates. Our Varian 936-70SP reads leak rates to 1 × 10⁻⁸ cc/sec.
- Non-destructive hermeticity check
- Varian 936-70SP leak detector
- Readings to 1 × 10⁻⁸ cc/sec
- Done in-house after welding
Some materials and material combinations don't have an established welding procedure yet. For those, we start with a sample weld, then cross-section, polish, and etch it to evaluate the weld before production. Additional operations such as heat treating and non-destructive testing can be carried out under our supervision.
- Sample weld before production
- Cross-section, polish, and etch
- Penetration, profile, and fusion checked
- Heat treating and NDT under our supervision
If you're not sure which service your part needs, send us the print.
The first to bring electron beam welding to Houston
Ernest Wilson founded Electron Beam Technology in 1981 and brought electron beam welding to Houston. Today we're a weld-only shop with 30+ years of individual staff experience, welding for oil and gas tool and instrumentation manufacturers. We give companies access to EB welding that the cost of capital equipment, project duration, or lot size would otherwise put out of reach.
About EBT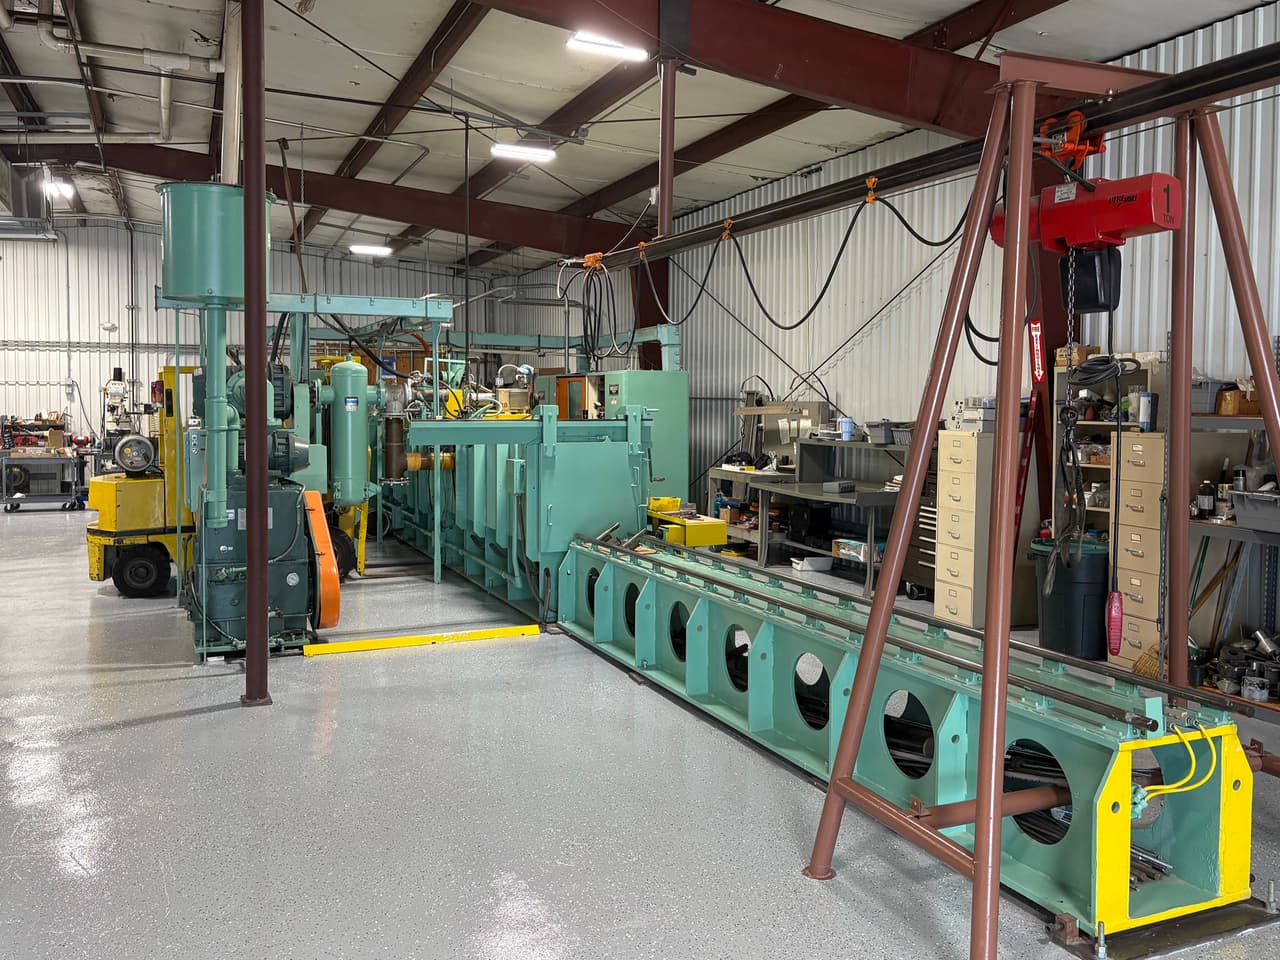
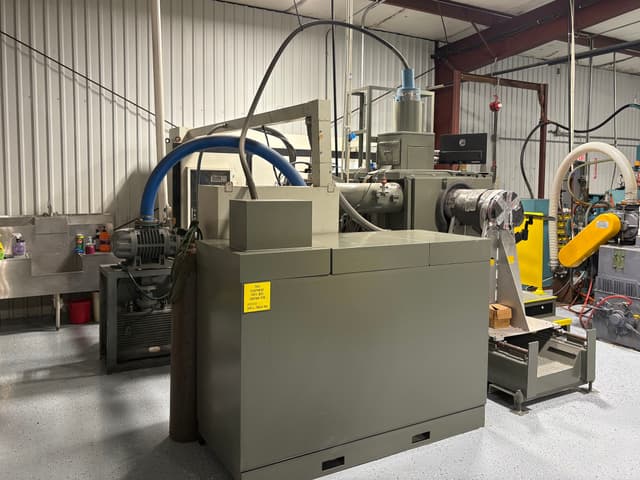
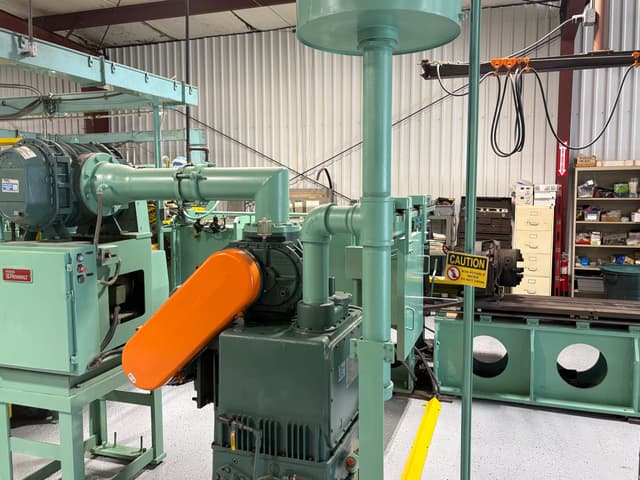
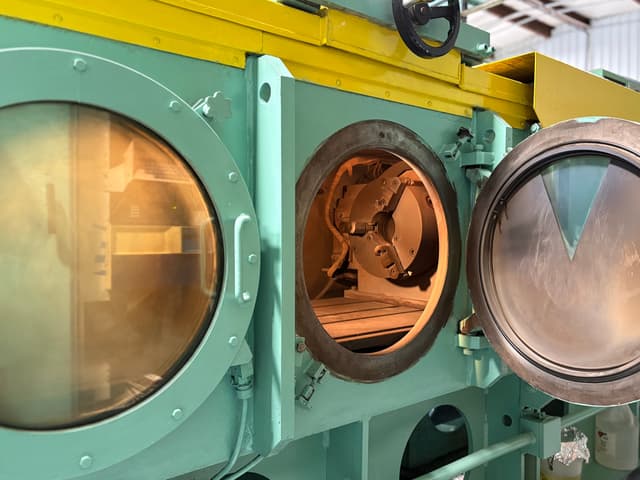
Three electron beam welders, from 0.010" to 6" deep
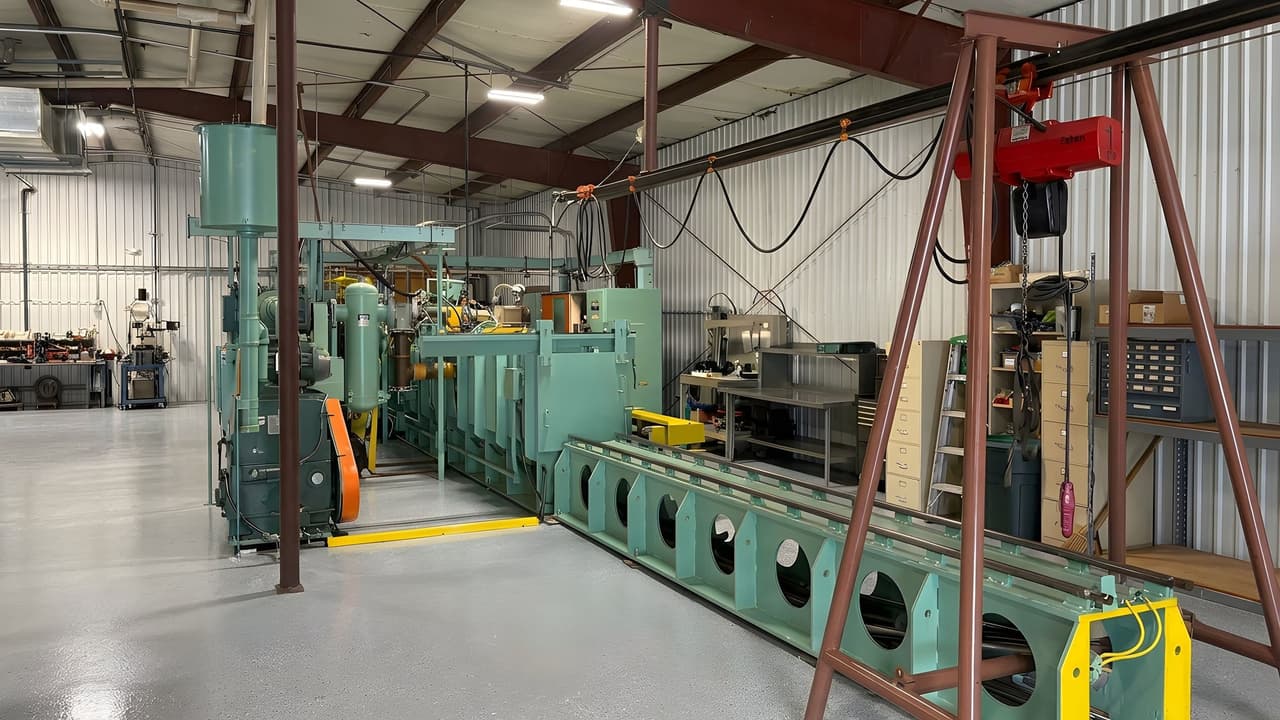
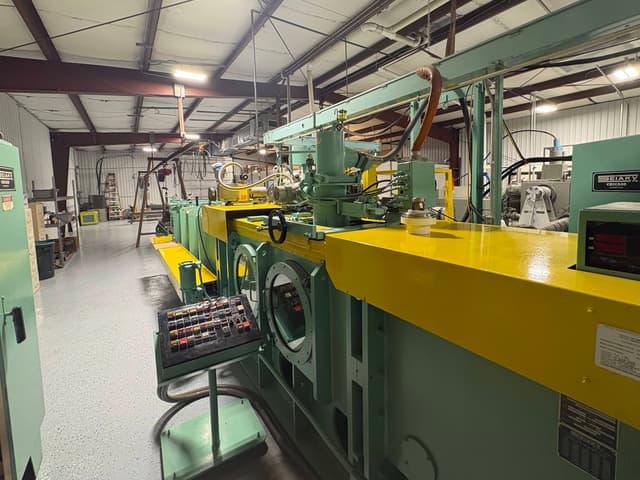
Sciaky electron beam welder
- Power
- 42 kW · 60 kV
- Part Length
- To 23.5 ft, depending on joint location
- Penetration
- .200" to 6"
- Weld Diameter
- To 11"
- Control
- CNC · variable penetration
Every weld is made in a vacuum
The vacuum keeps oxides and nitrides out of the weld zone. The electron gun is center-mounted, and the machine welds parts up to 23.5 ft long, depending on joint location.
CNC-controlled, repeatable welds
The Sciaky makes straight-line and circumferential welds with constant or variable penetration. Every welding parameter, including joint axis correction, is CNC-controlled and repeatable.
Crane handling for heavy parts
A crane handling system moves large, heavy components, such as long downhole tool housings, in and out of the machine.
Pumped down before welding
The pumps evacuate the chamber before welding. With no shielding gas or filler metal, the joint is fused cleanly from the parts' own material.
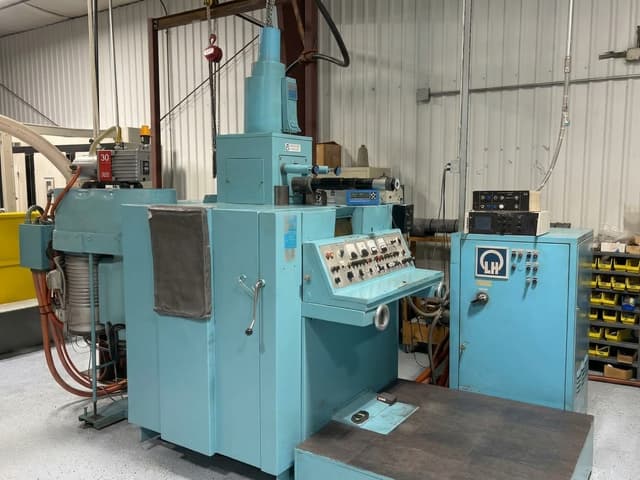 Precision · Batch Production · 150 kV
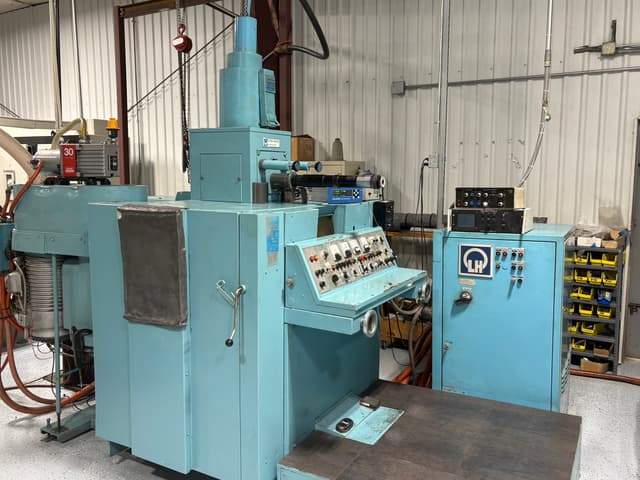
Leybold Heraeus electron beam welder
- Control
- Manual
- Chamber
- 36" W × 42" H × 52" L, plus extension
- Fixture
- Single-position or 24-chuck Ferris wheel
- Weld Diameter
- To 3.5"
- Penetration
- 0.010" to 1.00"
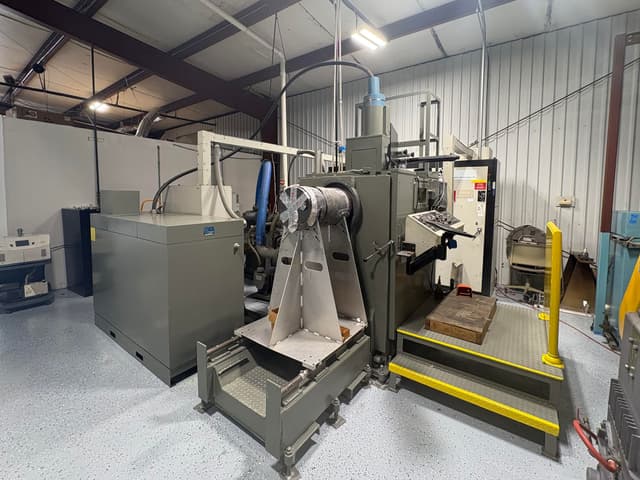 Precision · Rotary · 150 kV
PTR electron beam welder
- Chamber
- 36" W × 53" H × 55" L
- Motion
- Computer-controlled X-Y table + Z axis for rotary welding
- Part Diameter
- To 5"
- Deflection Welding
- Parts up to 37" tall
- Penetration
- 0.010" to 1.00"
- Spot Welding
Miyachi Unitek spot welder
- Type
- Precision resistance spot welding
- Controls
- Current, pressure, and weld time
- Leak Testing
Helium leak detector
- Model
- Varian 936-70SP
- Leak Rate Readings
- To 1 × 10⁻⁸ cc/sec
If your drawing calls out an EB weld, send us the print for a quote.
Request a QuoteWe test the weld on a sample before production
When a material or combination has no established welding procedure, we start with a sample weld and check it before any production parts are welded.
- 01
Sample welding
A test piece is welded to the callout on your drawing.
- 02
Cross-sectioning
The sample is cut through the weld.
- 03
Polishing
The cut face is polished for a clear view of the weld.
- 04
Etching
Etching makes the weld depth and fusion zone visible.
- 05
Weld evaluation
We evaluate the weld, then send the sample to you to verify.
Deep, narrow welds with low heat input
Electron beam welding is a fusion welding process. A focused beam of high-speed electrons melts and fuses the joint inside a vacuum chamber, with no filler metal or shielding gas. On our CNC Sciaky, every welding parameter is programmed, so each part in a run gets the same weld.
- Accuracy
- Economical
- Repeatability
- Light penetration
- Deep penetration
- Large and small parts
- Low heat input
- Low distortion
| Attribute | Electron Beam | Laser | TIG / Arc |
|---|---|---|---|
| Depth-to-width ratio | 12:1 to 30:1 | Up to about 10:1 | Wide, shallow bead |
| Heat input | Low | Low | High |
| Distortion | Low | Low | Higher |
| Single-pass depth | Over 4" (6" on our Sciaky) | About 1" | About 1/8" |
| Dissimilar metals | Many combinations, when compatible | Some combinations | Limited |
| Atmosphere | Vacuum | Shielding gas | Inert shielding gas |
| Repeatability | CNC, recorded parameters | Automated | Operator-dependent when manual |
Indicative values for comparison. Results vary by material, joint, and machine.
Materials we weld
Our experience includes a broad range of high-performance and specialty alloys.
- Inconel
- Incoloy
- Hastelloy
- Titanium
- MP35N
- Beryllium copper
- Nitronic 50
- Ask about your alloy
New or challenging materials
If an alloy has no established welding procedure, we develop one from a sample weld and evaluate it before production.
Our development processJoining dissimilar metals
EB welding is particularly well suited for joining many combinations of dissimilar metals. When the materials are compatible, the concentrated beam gives close control of heat input at the joint.
Send us your print
Quotes are typically returned within 1 day. Include the material, quantity, and the date you need the parts.
PDF · DWG · DXF · STEP · JPG · PNG
- Phone (713) 690-2326
- Email info@beamweld.com